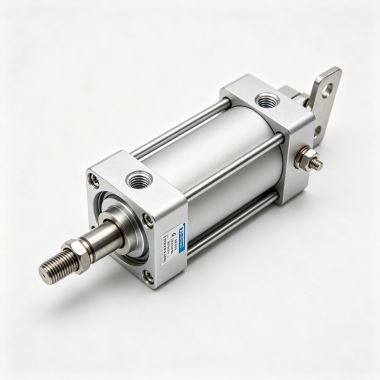


Description: Belt Tracking Cylinder (filter belt tracking cylinder / automatic deviation correction cylinder) is pneumatic actuator executing automatic offset correction for corn gluten belt filter press, key spare part governing filter belt running control. During belt filter press continuous operation, uneven belt tension, material distribution offset and roller surface wear will induce filter belt lateral mis tracking. Un corrected offset tracking will cause filter belt edge abrasion tearing, material spillage and secondary equipment damage. Receiving mis tracking detection signal, belt tracking cylinder drives tracking roller to perform left right swinging motion; real time adjusting filter belt travel trajectory and constraining belt operation along central reference line.
Cylinder barrel: Aluminium alloy tubular housing containing internal piston assembly.
Piston & piston rod: Moving components transforming compressed air pressure energy into linear thrust output.
End caps: Front and rear end covers fitted with air port connections and built in buffer dampening assemblies.
Sealing components: Piston seal rings, piston rod dust exclusion seals; preventing air leakage and water intrusion.
Magnetic proximity switches: Externally mounted sensors detecting piston position and feeding back deviation feedback signal.
Mounting hardware: Rear hinged bracket plus front spherical rod end connector for linkage connection toward tracking mechanism.
Auxiliary fittings: Flow control connectors and air hose interfaces for cylinder motion speed adjustment.
Co operates with offset detection hardware to realise closed loop automatic belt tracking:
1. Mis tracking detection: Photo electric or pneumatic probes are installed on both filter belt sides. When filter belt drifts sideways and touches probe element, deviation feedback signal is triggered.
2. Solenoid valve reversing: Upon receiving offset signal, PLC actuates 2 position 5 way solenoid valve for air circuit commutation; compressed air feeds into selected cylinder chamber.
3. Cylinder thrust actuation: Piston rod extends / retracts, pushing tracking roller to swing angular displacement around fulcrum pivot.
4. Filter belt correction: Angular deflection of tracking roller generates lateral guiding force; gradually steers mis tracked filter belt back toward central position.
5. Automatic reset: After filter belt returns to normal running position, probe signal resets; cylinder rod returns to neutral stroke completing correction cycle.
Agile response: Fast pneumatic actuation enabling rapid offset correction action.
Appropriate thrust magnitude: Output thrust sized for filter belt correction requirement without inflicting belt damage.
Smooth end stop behaviour: Integrated buffer dampening eliminates mechanical impact at stroke end positions.
Simple installation: Standard cylinder dimensional spec with hinged mount style, high component interchangeability.
Robust sealing performance: Dust proof water proof sealing rings suited for humid splashing work environment.
Adjustable parameters: Stroke length and actuation speed configurable to match varying filter belt width specifications.
Extended service life: Aluminium alloy cylinder barrel anti wear construction; sealing sets deliver long operational cycles.
 Contact Us