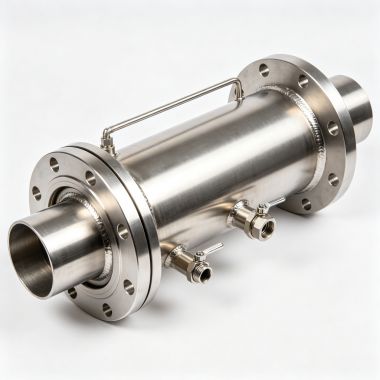


Description: Also known as pipeline auxiliary air injector / air replenisher / air booster. Auxiliary air makeup hardware installed midstream of long distance cornstarch pneumatic conveying pipelines; critical sparepart securing stable longhaul conveying. During long distance transport, progressive pipeline pressure loss reduces airstream velocity. When velocity drops below particle suspension speed, starch powder settles on pipe bottom and causes blockages. Air booster injects supplementary compressed air to restore pipeline pressure and flow velocity, preventing material sedimentation and pipe plugging for reliable long distance conveying.
Main body shell: Cylindrical stainless steel housing with flange ends for series connection to main conveying pipeline.
Venturi nozzle: Core jet element with converging diverging flow path accelerating compressed air to supersonic velocity.
Air inlet port: Side mounted connection for compressed air branch line, fitted with shutoff valve and filter.
Diffuser section: Gradually expanding outlet segment enabling smooth airflow velocity transition and reduced flow resistance.
Flow deflector: Internal rectifier homogenising mixing between makeup air and main stream flow.
Inspection port: Access for nozzle and internal flow path cleaning against blockages.
Operation follows Venturi jet ejector physics:
1. High pressure air intake: Filtered compressed air (0.4–0.7 MPa) enters air booster via sideport.
2. Nozzle acceleration: Compressed air passes converging nozzle; pressure energy converts into kinetic energy reaching supersonic velocity.
3. Ejector mixing: High speed jet generates negative pressure inside mixing chamber, entraining and accelerating material laden main stream airflow for thorough mixing.
4. Diffuser pressure recovery: Mixed flow enters diffuser section; velocity decreases while static pressure recovers, restoring conveying pressure and flow velocity inside main pipeline.
5. Anti blockage effect: Upon material sedimentation and pipeline pressure rise, booster injects supplementary air to propel material forward and avoid pipe clogging.
Excellent anti blockage performance: Compensates pressure loss for long distance conveying and inhibits starch sediment caused plugging.
Zero moving internals: High operational reliability and minimal maintenance demand.
Food grade material: 304 stainless steel construction, polished innerwall complying with food hygiene specifications.
Fast response: Compressed air actuation delivers immediate pressure recovery.
Low additional flow resistance under normal conveying conditions.
Simple flange series installation, no major modification required for existing piping layout.
Automatic control capable: Interoperates with pressure transmitters and solenoid valves to realise autonomous air makeup logic.
 Contact Us